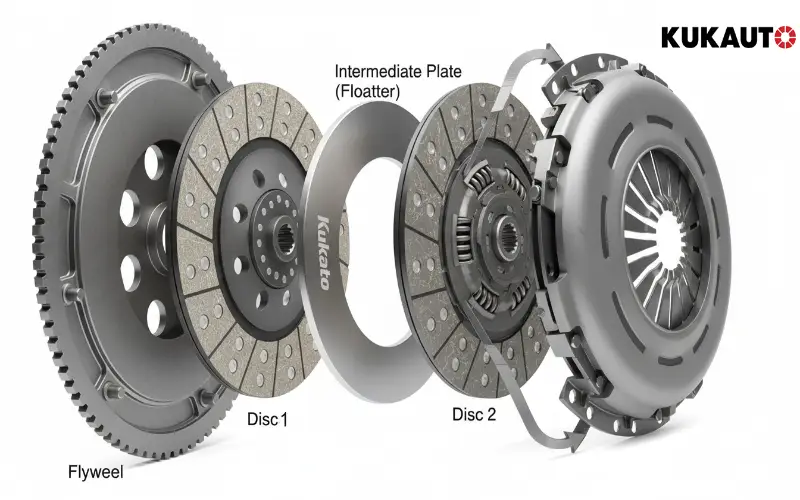

Sourcing OEM mining clutch kits is far more than simply matching specifications or comparing prices. It requires careful evaluation of product quality, manufacturing capability, and the supplier’s ability to deliver consistent performance over the long term. Among all the factors buyers should assess, test reports are one of the most reliable indicators of a product’s true quality. But what should you look for in a test report, and which results matter most? In this article, we’ll walk you through the key points every OEM buyer should verify before making a sourcing decision.
Most procurement advisors tell you to check the supplier’s ISO certificate. Em 2026, essa mentalidade ainda queima frotas. Um certificado ISO por si só não verificará a qualidade da embreagem de mineração – ele lhe renderá uma pilha de papelada enquanto um caminhão de transporte fica parado em um declive. Um gerente de frota de uma mina de cobre chilena aprendeu isso da maneira mais difícil, depois que um pedido de embreagem de US$ 50 mil derrubou a promessa da amostra de pré-produção. A amostra foi testada lindamente e o preço FOB ficou bem abaixo do próximo licitante, então o pedido passou pela aprovação da amostra. Três meses depois, todas as unidades de produção em massa começaram a falhar sob carga total. O culpado? A linha de produção trocou discretamente o material do disco de fricção por um composto que amolecia a 480°C, e não aos 620°C que a amostra atingiu. Ninguém listou essa tolerância de qualidade no contrato. Nenhum certificado detectou isso porque ninguém exigiu um relatório metalúrgico específico do lote.
When you source heavy-duty kits for a mine fleet, the real filter isn’t a wall of certifications. It’s whether a supplier can hand you a 1‑million‑cycle servo‑hydraulic fatigue test with clamp‑load loss under 5%, torque‑signature logs from automated nut‑runners, and thermal‑imaging proof that the friction disc holds above 600°C through the whole heat cycle. Those five validation gates—along with how to read the reports and spot a low‑grade kit before it kills uptime—are what the rest of this article unpacks.
The Cost of Trusting a Certificate Alone
Certificates prove a factory passed an audit; they don’t prove your batch survives 3000 kg clamp load for 1 million cycles.
Every procurement article tells you to check for ISO certification first. That’s lazy advice. A certificate only confirms a management system existed during a snapshot audit. It says nothing about whether the pressure plate castings in this shipment contain micro-porosity that will crack under 3000 kg of repetitive clamp force, or whether the assembly line actually torqued every bolt to the same value. Trusting a certificate alone is how a $50,000 order turns into 14 days of haul truck downtime.
A inspeção visual deixa de funcionar na manipulação das embreagens de mineração de cargas. Os dedos da mola do diafragma parecem idênticos a olho nu, mas pequenas variações de espessura de 0,2 mm criam uma distribuição assimétrica do grampo. Abaixo de 3.000 kg, isso se traduz em uma diferença de carga de 10–15% na face do disco. O resultado: desgaste irregular, pontos quentes e vibração que destroem os rolamentos do eixo piloto da caixa de engrenagens – tudo invisível na inspeção.
The number one cause of premature aftermarket clutch failure in mining fleets is inconsistent assembly torque. When cover bolts are tightened manually or with uncalibrated pneumatic tools, variation reaches ±20%. That scatters the preset clamp load, causing the clutch to engage unevenly. Hot zones form, warping the pressure plate and glazing the friction material. Within 800–1000 hours, you get chattering disengagement and cracked hub springs. You eliminate this failure mode instantly by requiring torque-signature logs from automated nut-runners—every bolt, every assembly, proven identical.
A static load test is a worthless green checkmark. Most budget suppliers clamp the cover in a press, apply 3000 kg once, and call it tested. A genuine OEM-grade clutch must pass a servo-hydraulic fatigue test: 1 million full-load cycles, clamp force loss ≤5%, and thermal imaging run-out showing uniform temperature distribution. Without that report, you’re gambling on a part that hasn’t proven it can survive a single year in a Komatsu 930E.
Check the friction disc metallurgy report for sustained temperature tolerance. Organic-based aftermarket discs fade above 450°C. A heavy hauler descending a ramp with a full load generates disc temperatures exceeding 550°C repeatedly. The spec you need is ≥600°C sustained without permanent coefficient of friction loss, typically from a ceramic-metallic formulation. If the supplier can’t name the fade threshold, it’s a generic light truck disc relabeled for mining.
-
- Servo-hydraulic fatigue report: 1 million cycles, ≤5% clamp load drop for your specific part number.
- Torque-signature logs: Multi-spindle automated nut-runner data showing <3% bolt-to-bolt variation.
- Metallurgy certificate: Friction disc core temperature tolerance verified above 600°C sustained.
| Certificate or Claim | Hidden Assumption | Cost of Trusting It Alone | Hard Proof to Demand Instead |
|---|---|---|---|
| Generic ‘ISO 9001’ or ‘OEM Quality’ Certificado | Implies full lifecycle engineering, but often only covers basic quality management. No proof of high-stress metallurgy or fatigue life. | Catastrophic downtime from premature disc disintegration under 3,000 kg clamp loads that visual inspection cannot detect. | Batch-specific Metallurgy Report with friction disc core temperature tolerance data. |
| Static Pressure / Load Test Report | Assumes a one-time axial force check equals dynamic reliability over a truck’s entire service life. | Clamp load collapse >30% within months, causing slippage, warped plates, and burnt flywheels under cyclic haulage stress. | 1-Million-Cycle Servo-Hydraulic Fatigue Test proving clamp force loss stays ≤5% from start to finish. |
| Standard Factory Assembly Report | Hopes that manual bolt tightening is ‘close enough’ to uniform, ignoring micro-variable friction at each thread. | Uneven clamp distribution creates thermal runaways and hot spots on the pressure plate, leading to vibration-induced dowel failure. | Automated Torque-Signature Logs from calibrated nut-runners, proving identical tightening angles on every single bolt. |
| Basic Friction Material Datasheet | Lists room-temperature coefficient only, ignoring radical fade characteristics during sustained high-torque mining operations. | Clutch glazing and complete friction loss after a downhill loaded retarder cycle, when core temps routinely exceed 600°C in rigid dump trucks. | Batch-Specific Coeficiente de fricção Curve under sustained 600°C+ heat, with thermal imaging run-out and clamp-load retention analysis. |
| ‘Balancing’ Mentioned Without Data | Static balancing on a knife-edge rig is considered sufficient for high-RPM diesel powertrains. | Harmonic vibrations destroy input shaft bearings and cause driveline fatigue, requiring unscheduled major overhauls. | Dynamic Balance Test results at operational RPM, certified to at least G6.3 grade or stricter per OEM requirements. |

5 Validation Tests Every Supplier Must Provide
Forget the generic ISO cert.
A $50,000 order was scrapped because
1. Servo‑hydraulic fatigue test (1‑million‑cycle report). Most shops only run a static clamp load test. That’s worthless for a rigid‑frame mining truck that sees 100,000 engagement cycles a year. You need a full 1‑million‑cycle endurance run on a servo‑hydraulic test stand. The pass criterion: clamp load must not drop more than 5% from the initial 3,000–3,200 kg specification. Anything worse and you’ll see slippage and burn‑out before the second engine overhaul.
2. Metallurgical analysis for plate and disc materials. Don’t accept a sales sheet that says ‘high‑grade steel.’ Request a separate lab report showing the friction disc core material can tolerate sustained temperatures above 600°C. Mining clutches routinely soak at 450–550°C on long hauls; a disc that starts to oxidize or lose friction coefficient at 400°C will fail inside a quarter. Also verify the pressure plate grade—G250 gray iron or better—and ask for the heat treatment curve.
3. Assembly torque‑signature logs from automated nut‑runners. Manual torque wrenches introduce a ±15% scatter, which creates uneven finger pressure and hot spots that warp the disk. Demand the digital torque‑signature log for each assembled unit. It proves every bolt was tightened to the exact same angle and final torque, usually within a 2% tolerance band. If the supplier can’t provide individual unit logs, assume they’re hand‑tightening on the floor.
4. Thermal imaging run‑out cycle with clamp‑load retention. A proper test runs the clutch assembly through a series of engagement/disengagement cycles while an infrared camera maps the temperature distribution. You’re looking for even heat dissipation and no hot bands that indicate warpage. At the end of the cycle, clamp load should still be within 90% of the cold value. If the supplier can’t produce a time‑stamped thermal image sequence, the run‑out wasn’t done.
5. Batch‑specific friction coefficient under sustained heat. Friction formulations can drift between production lots. Require a test report from each batch where the dynamic friction coefficient is measured at a sustained 500°C for at least 10 hours. The coefficient must stay within the OEM spec window—typically 0.32–0.38 for sintered metallic pads—and the wear rate must be documented. Without this, you’re gambling that the next shipment performs like the approval sample, and that’s exactly how an $80,000 rebuild turns into a 2‑week downtime event.
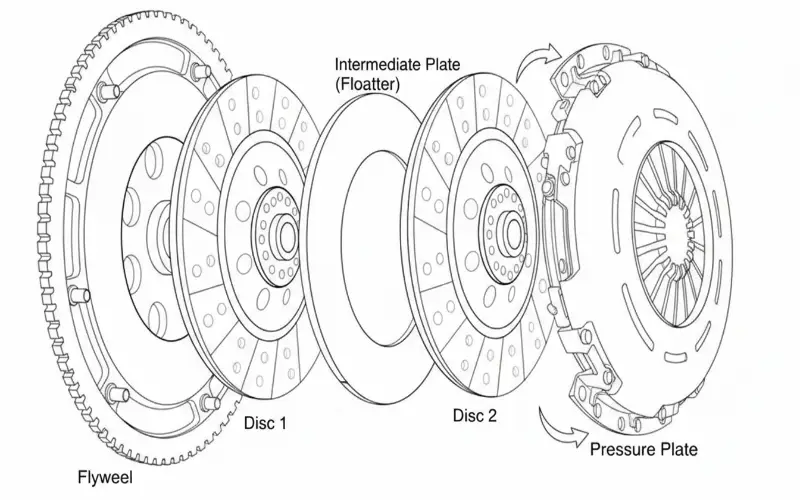
How to Read a Clutch Test Report
Clamp load loss ≤5% after 1M servo‑hydraulic cycles is the hard line between a clutch that outlives the truck and one that.
A 5% clamp force drop after 1 million fatigue cycles isn’t an arbitrary number. It mirrors the full lifecycle of a rigid dump truck—roughly 18,000 operating hours with 55 engagements per shift. In a Komatsu 930E ou Caterpillar 797, the OEM‑spec clutch clamp load sits around 3,200 kg. A 5% loss—160 kg—shrinks torque capacity by nearly the same margin. On a 12% grade with a 290‑tonne payload, that deficit forces the clutch into partial slip long before the friction material is worn. Heat spikes follow. The flywheel micro‑cracks. And the failure cascade begins inside a single shift.
Cross‑referencing a supplier’s test report with haul truck OEM specs means reading past the summary page. First, pull the torque‑signature log from the automated nut‑runner line. Every bolt on the cover assembly should show tightening torque within ±3% of the engineering spec. Manual tightening creates ±15% variance—enough to generate hot spots that warp the placa de pressão by 0.15 mm, which you’ll later see as a pedal judder complaint. If the supplier won’t hand over these logs, they’re hiding inconsistent assembly.
-
- Metallurgy match: Demand a separate spectrographic analysis for the friction disc core and placa de pressão. O disco deve suportar temperaturas centrais sustentadas acima de 600°C. Verifique a matriz de carbono-silício na placa de ferro fundido cinzento com as especificações do material OEM – as substituições aqui causam trincas por fadiga térmica antes de 8.000 horas.
- Esgotamento da imagem térmica: O teste de ciclo térmico deve mostrar a retenção da carga do grampo após 500 ciclos da temperatura ambiente até 450°C da superfície. Um relatório sem fotos de câmera infravermelha – apenas uma ‘passagem’ stamp—is worthless. You need the delta‑temperature across the disc face. More than 20°C variation indicates uneven friction material distribution, leading to chatter in cold‑start operations.
- Friction coefficient under sustained heat: Batch‑specific friction coefficient graphs need to stay within OEM tolerance bands. For mining clutches, the dynamic coefficient should remain above 0.35 at 350°C. If the supplier’s report only shows room‑temperature data, they’re hiding fade problems that surface when a truck crests the pit ramp.
The final 10%: always check the sample approval protocol the supplier used. A proper pre‑production sample must be selected at random from the first production run, not hand‑built in a lab corner. If the sample approval sheet doesn’t reference the same batch number as the production test reports, you’re reading fiction. Walk away.
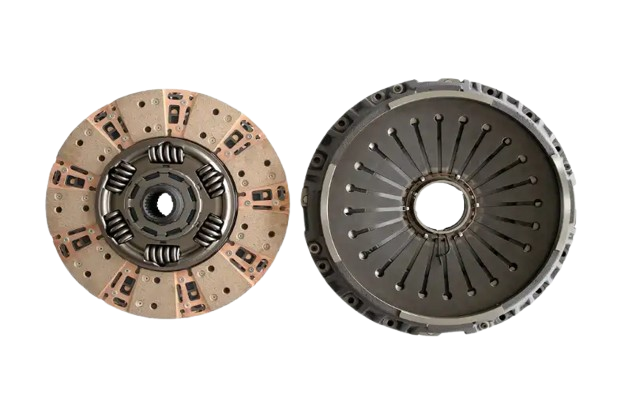

Red Flags That Signal a Low‑Grade Kit
If a supplier’s only quality proof is an ISO 9001 wall poster, walk away.
Missing batch logs are the number one tell. A legitimate supplier ships every kit with a serial-linked test data pack—clamp load curve, release bearing travel, and dynamic balance numbers. If the crate arrives with nothing but a packing slip and a photocopied “ISO certified” card, assume those clutches were assembled by feel, not by measurement. I’ve seen a $50,000 order where the production run had 23% lower clamp force than the approved pre-production sample, and the fleet manager only found out when three haul trucks limped off the pit with burnt discs in the same month. The supplier had no batch log to cross-reference because they never recorded it.
- Generic ISO claims: An ISO 9001 certificate proves a company has a documented quality management system. It says nothing about whether your specific clutch was tested. Demand IATF 16949 or a process audit report that covers the actual assembly line, not just the office.
- No dynamic balance data: A clutch cover assembly spinning at 2,400 RPM with even 60 g·mm of residual imbalance hammers the transmission input bearing. Any supplier that cannot produce a printout showing per-unit balance correction (to a tolerance of 15–30 g·mm at operating speed) is skipping a non-negotiable step.
- Absent material traceability: Friction discs must survive sustained 600°C core temperature. If there’s no heat-lot-traceable metallurgy report for the steel plate and friction material—citing exact alloy and coefficient of friction after thermal soak—you’re buying a mystery.
Suppliers who deflect a dynamic balance request with “our jigs ensure it” are red-flagging hard. Dynamic balancing isn’t a one-time setup check; it shifts with every small variation in pressure plate casting and mola do diafragma rivet tension. Without a per-unit balance report, the first warning you’ll get is a hairline crack across the flywheel housing after 3,000 hours. I’ve seen aftermarket kits where the balance error exceeded 100 g·mm—four times the OEM spec for a rigid dump truck. The repair cost wasn’t the clutch; it was a $14,000 transmission overhaul.
Another proxy test: ask for the correlation data between the pre-production sample approval and the first mass production run. If the supplier stalls or sends a blank stare, they probably can’t replicate the sample’s quality at volume. Real OEM-grade manufacturers keep a locked sample master and overlay batch torque-signature logs against it—every kit must fall within a defined quality tolerance band, typically ±3% on clamp load and release load. Anything wider, and you’re gambling.
Conclusão
A single premature clutch failure on a haul truck costs far more than the price difference between a validated kit and a low-grade copy. The engineering data—the 1‑million‑cycle fatigue log, the torque‑signature printout, the metallurgy report showing sustained heat tolerance above 600°C—separates a part that runs three full maintenance cycles from one that strands a truck on a 12% grade.
Next supplier call, pin down that 5% clamp‑load‑loss ceiling on the fatigue test. If they can’t produce a batch‑specific report with that number, you already have your answer. Browse the mining truck clutch solutions page to compare kits engineered to this benchmark.
Perguntas frequentes
What tests verify OEM-grade mining clutch quality?
Demand servo‑hydraulic fatigue test reports, metallurgical plate analysis, and automated assembly torque‑signature logs. A supplier unwilling to share batch‑specific data likely hides an aftermarket grade. Request all five validation tests before accepting any shipment.
How do I read a clutch fatigue test report?
Focus on clamp load loss after 1 million cycles. Anything above 5% means your mining truck could slip under peak torque, risking unplanned downtime. Use ≤5% clamp load loss as your go/no-go line.
What are red flags in a clutch kit supplier?
Certificações ISO genéricas sem registros específicos de lote, falta de resultados de equilíbrio dinâmico e sem registros de esgotamento de imagens térmicas. Essas lacunas quase sempre precedem as falhas iniciais em campo. Rejeite qualquer cotação que não possua evidências de teste em nível de lote.
Por que é necessário um teste de fadiga de ciclo 1M?
Ele reproduz anos de carregamento de choque em um caminhão de mineração em poucos dias. Sem ele, você estará apostando na fadiga do material que pode fraturar a mola do diafragma no meio do turno. Aceite apenas relatórios de plataformas servohidráulicas calibradas.
Qual limite de retenção de carga de fixação é importante?
Uma retenção de pelo menos 95% após ciclos térmicos e mecânicos sustentados separa os kits de qualidade OEM dos kits de baixo custo. Qualquer coisa menos reduz a vida útil da embreagem em até 40%. Confirme os dados do ciclo de esgotamento da imagem térmica antes de fazer o pedido.